Another vzbot235 from the community but with a metal z-axis. Default test settings.

I would like to point out that the new method of resonance generation (sweeping) is very good for trapezoidal screws that have play in the nuts, and without it the measuremets is distorted. I’m not sure if it’s them exactly, but it’s likely.
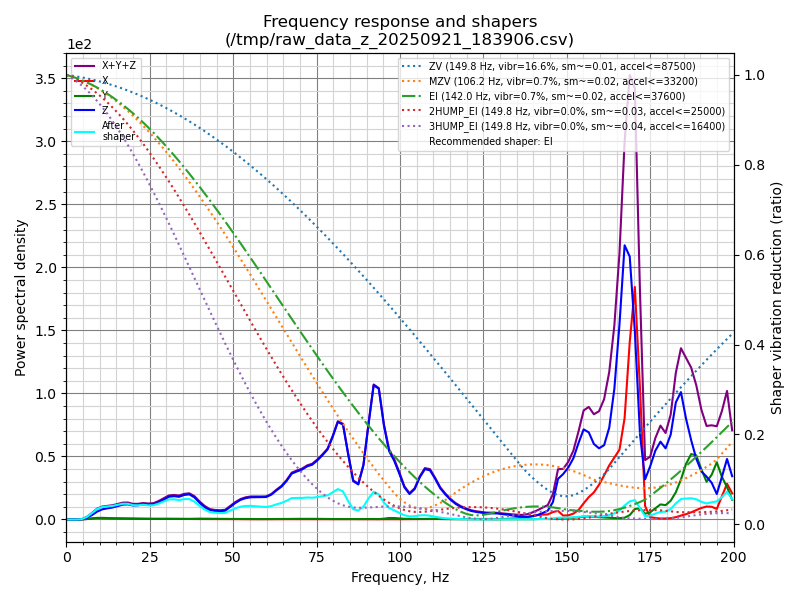

I would say that this is still low, and I would like to see a clear 1e3, but as you can see the peaks are clearly visible, and in any case we will not be able to find the optimal value for all printers, I think that accel_per_hz_z=15 is a good default/starting point.
Issue:
If you turn off shaping for the z-axis via SET_INPUT_SHAPER, the report message does not label this axis.

I think the problem is somewhere here.